
- Technology explained – technology and procedures
Weld testing: what the eye sees – and what only test methods find
By Tobias Schott · 5-minute read · Updated November 2026
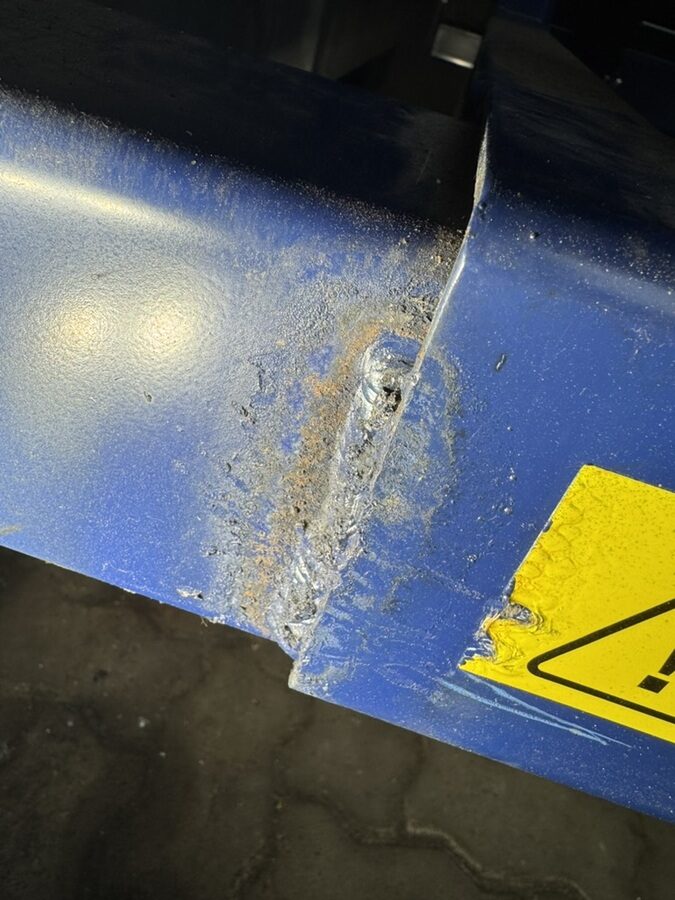
Weld testing checks whether a weld is free of cracks, porosity and lack of fusion – first by eye, then with methods such as dye penetrant, magnetic particle or ultrasonic testing, which also reveal fine and internal defects.
A weld can look clean from outside and still not carry. A fine crack, a pore inside or a side wall that has not fused properly remain invisible – until the weld gives way under load. That is why load-bearing welds are tested: during manufacture, after repairs and during periodic inspections.
Here we explain which defects occur in welds and how to find them with visual testing, dye penetrant, magnetic particles and ultrasound.
What is weld testing?
Weld testing is the inspection of a weld for defects that impair its strength or tightness. Testing is usually non-destructive – the component remains undamaged. The methods have international abbreviations: VT for visual testing, PT for penetrant testing, MT for magnetic particle testing, UT for ultrasonic testing and RT for radiographic testing.
Which test is needed depends on the component, the load and the specification. For simple repairs, visual testing is often enough; for load-bearing and highly stressed welds, further methods are added.
There are also destructive tests: a specimen is bent, pulled or cut open. This is done when qualifying welders and welding procedures on test pieces, not on the finished component. For plants in operation, the non-destructive methods are what matters.
Key facts
- Aim: Find cracks, porosity, lack of fusion and shape defects.
- Visual testing (VT): always the first step, for everything on the surface.
- Dye penetrant testing (PT): fine surface cracks, on almost all materials.
- Magnetic particle testing (MT): cracks at and just below the surface, magnetic steel only.
- Ultrasonic (UT) and radiographic testing (RT): defects inside the weld.
- Who tests: trained staff; certified inspectors for formal evidence.
Which defects are there?
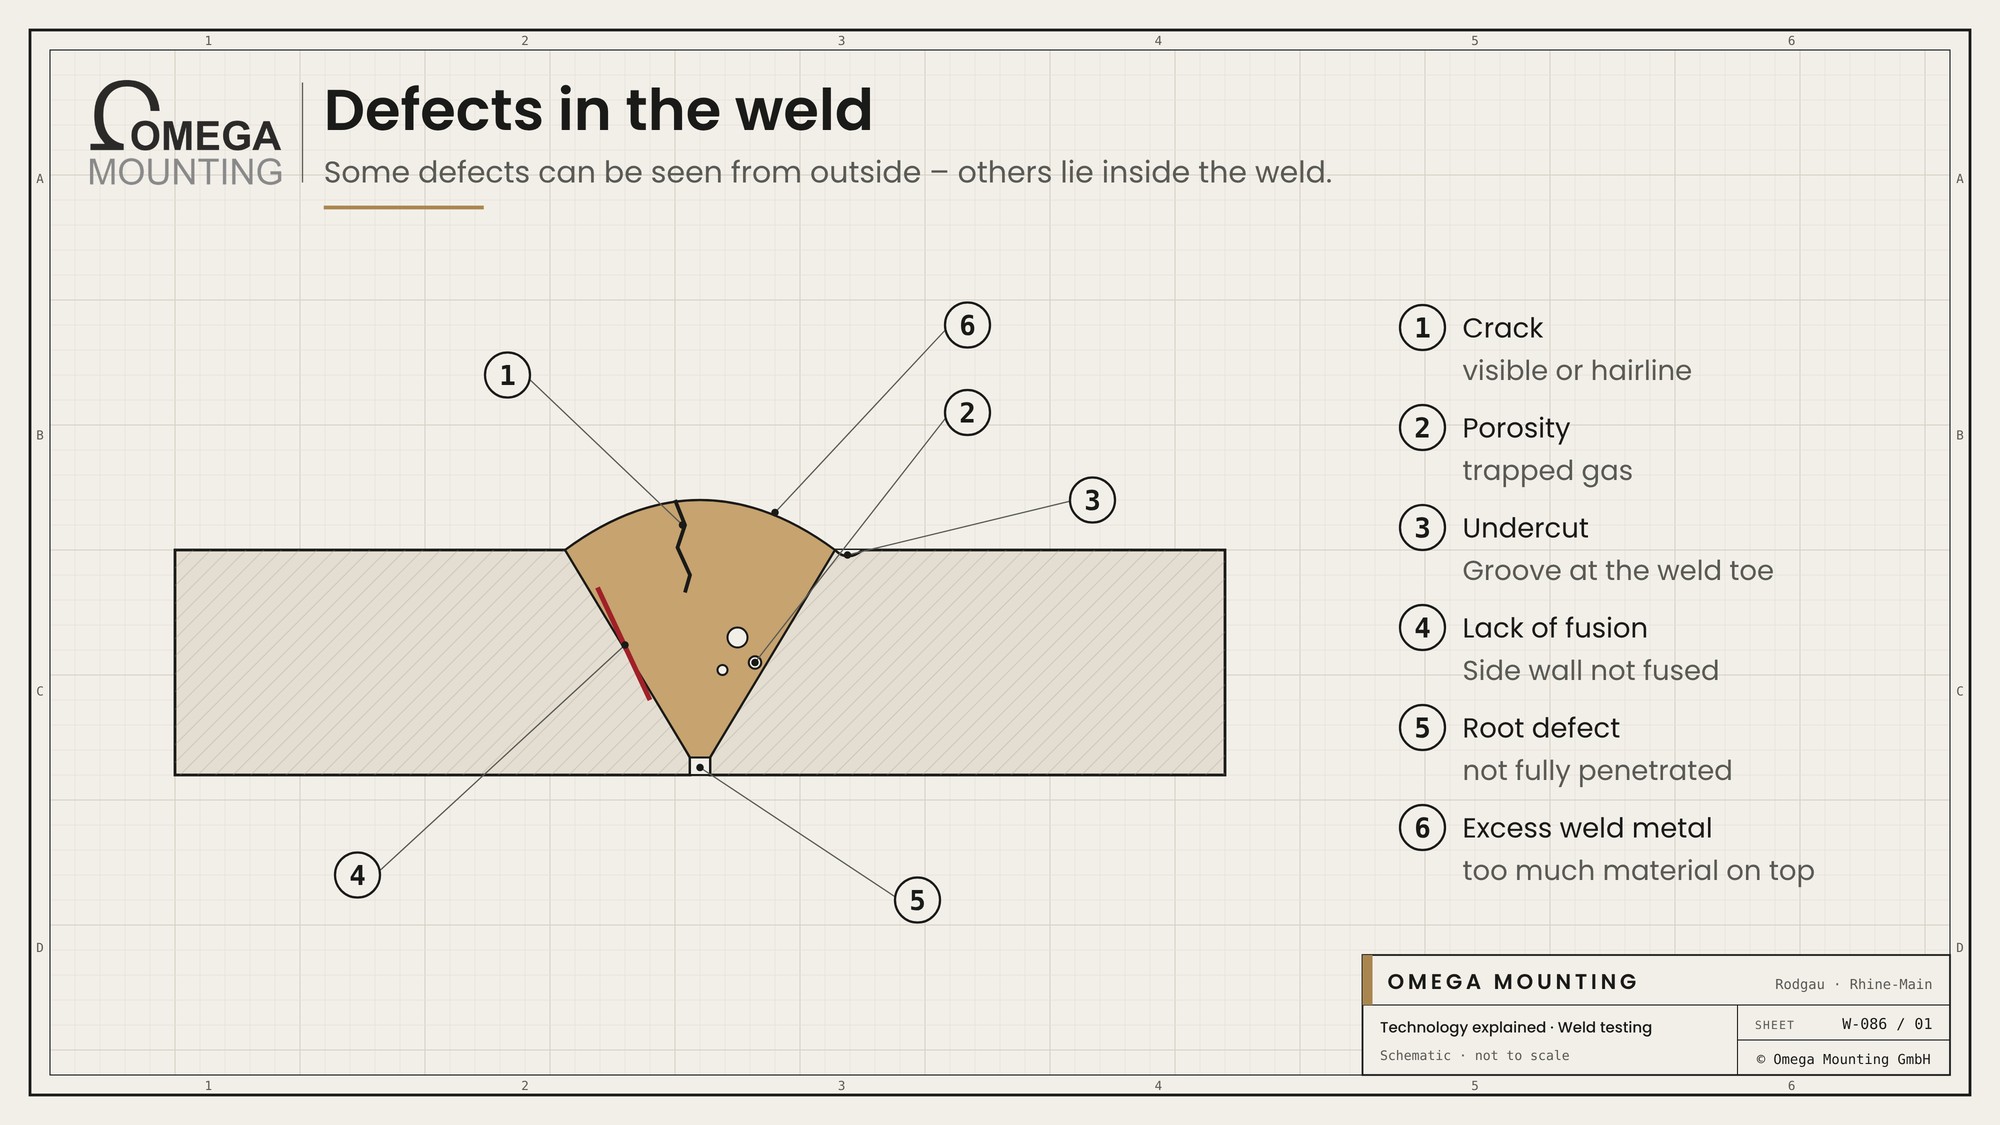
Welding defects can be told apart by where they lie.
- Crack: the most dangerous type of defect, often finer than a hair, caused by stresses or load cycles.
- Pore: trapped gas, single or in clusters – often caused by dirt, moisture or missing shielding gas.
- Undercut: a groove at the weld toe where stresses concentrate.
- Lack of fusion: the weld lies against the side wall but is not fused with it – invisible from outside.
- Root defect: the weld is not fully penetrated, a gap remains at the bottom.
- Excess weld metal: too much material on top – looks strong but forms a notch at the transition.
Visual testing finds cracks, notches and excess weld metal. It does not find lack of fusion and internal pores.
Dye penetrant testing

Dye penetrant testing makes fine surface cracks visible – on steel, stainless steel and aluminium.
- Clean: The weld is made bare and grease-free.
- Penetrant: A red, thin liquid is sprayed on and is drawn into every crack by capillary action.
- Intermediate cleaning: The excess is wiped off the surface – the penetrant stays in the crack.
- Developer: A white layer draws the penetrant back out of the crack. The crack appears as a red line on a white background.
The method is simple, needs little equipment and is well suited to use on site. But it only finds defects that are open to the surface. Paint, rust or scale must be removed completely beforehand, otherwise the crack stays closed.
Magnetic particle testing
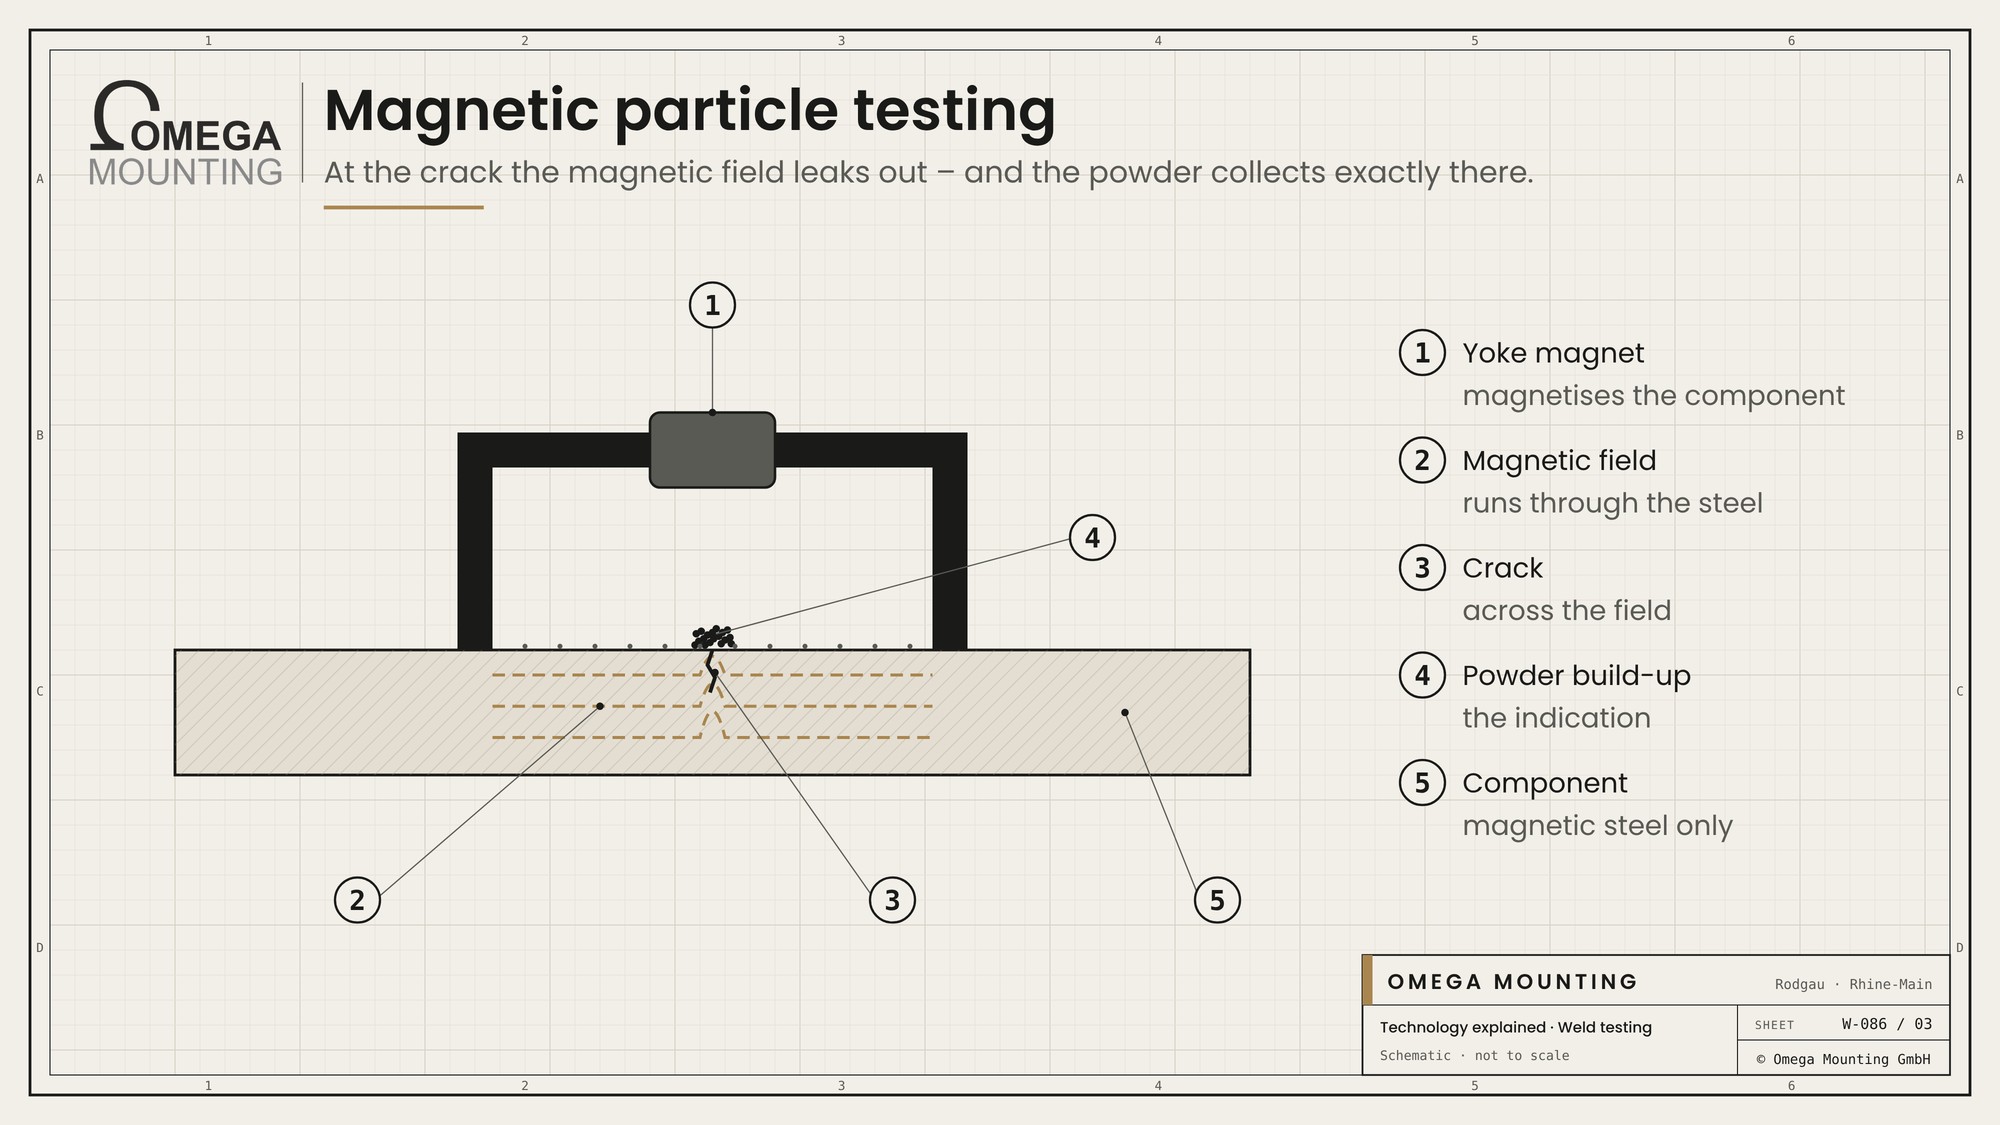
On magnetisable steel, magnetic particle testing finds cracks at and just below the surface.
- Magnetise: A yoke magnet creates a magnetic field in the component.
- Field leaks out: Where a crack lies across the field, the field leaks out of the surface.
- Powder collects: Sprayed-on magnetic powder, often fluorescent, collects exactly there.
- Two directions: Because only cracks across the field become visible, testing is done in two directions.
The method is more sensitive than penetrant testing and also finds cracks closed by paint or dirt. It does not work on stainless steel and aluminium.
Ultrasonic and radiographic testing
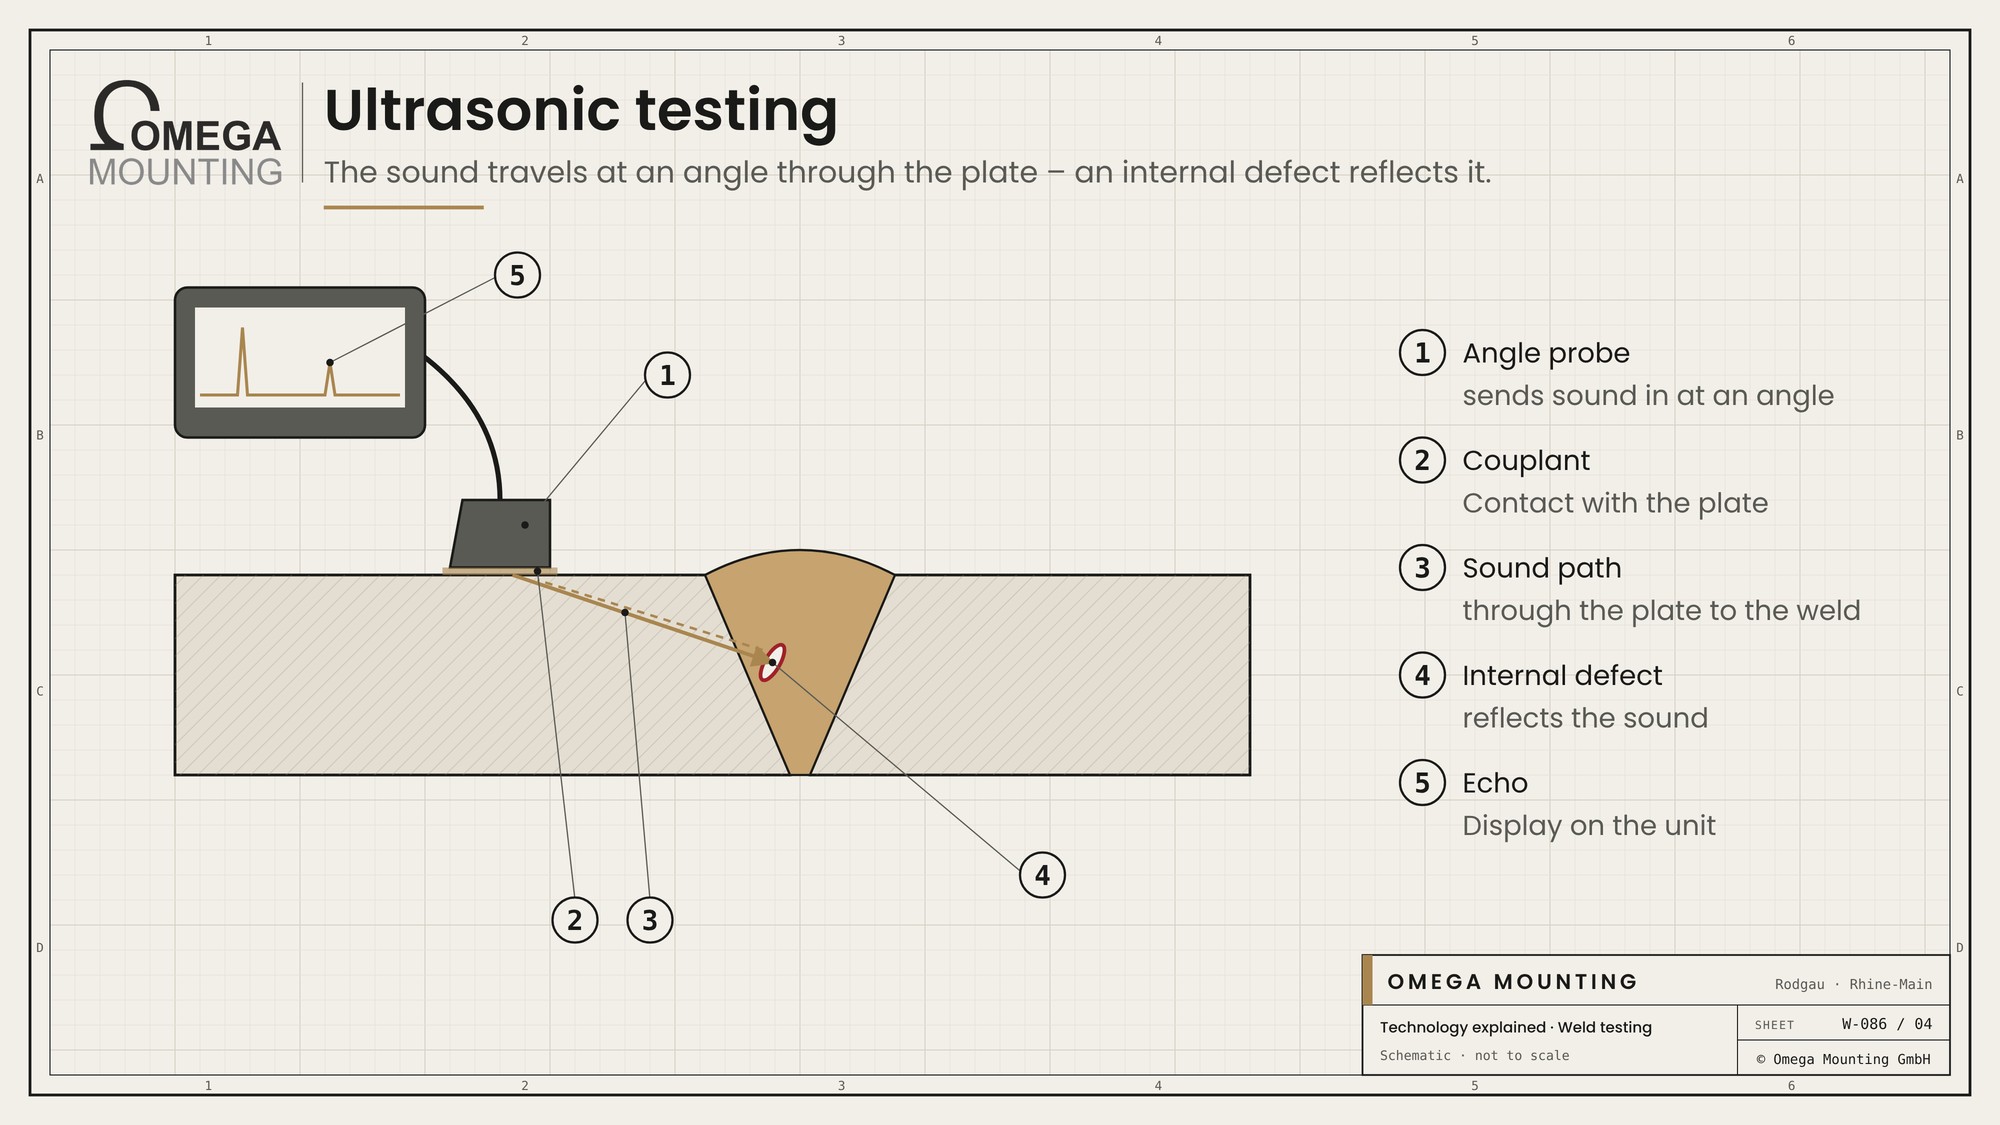
Only methods that see through the material find defects inside the weld.
- Ultrasonic: A probe sends sound at an angle into the plate. If it hits a defect, it is reflected and appears as an echo on the screen. A couplant ensures contact between probe and plate.
- Radiography: X-rays or gamma rays pass through the weld and expose a film or detector. Pores and lack of fusion show up as dark areas. Because of the radiation, a cordoned-off area is needed.
Both methods belong in the hands of certified inspectors. Who may carry out which inspection on installations is explained in our article on the competent person.
Planning and documenting inspection
Which weld is inspected and how is ideally decided before welding. For installation this means:
- Know the scope: The drawing or inspection plan states which welds are inspected and how many.
- Accessibility: Inspectors need access to the weld, often from both sides. Scaffolds and platforms stay until inspection.
- Surface: For dye penetrant and magnetic particle testing the weld must be clean and free of spatter.
- Timing: Some materials are only inspected after a waiting time because cracks can form with a delay.
- Weld numbers: Every weld gets a number so findings and repairs can be clearly assigned.
Qualified inspectors carry out the testing itself. Installation makes sure they can test and repairs any findings. After a repair the same spot is inspected again – only then is the weld complete.
What we pay attention to
Testing starts with welding, not afterwards.
- We look at every weld ourselves during and after welding.
- We grind out cracks completely before re-welding – if needed with a penetrant test to confirm the crack is gone.
- We weld with deep penetration and avoid notches at the weld toe.
- We document repair welds with photos before and after.
- We agree with the inspector which test the follow-up inspection requires.
Where we use it
At a loading dock, during the statutory inspection the inspector had rejected the welds – no sticker, door closed. We ground out the defective welds and re-welded them so that the dock could be released again at the follow-up inspection. How a defect is rectified before the follow-up inspection is described in our guide Rectifying UVV defects.
On the tubular shaft of a cable drum at an inland port on the Main cracks had formed due to incorrect slinging. We ground them out completely and rebuilt the shaft with repair pieces.
More technology explained
Technology explained
which weld is tested.
Technology explained
what the weld is made with.
Technology explained
who inspects.
Do you have questions about how this works on your site?
Has your installation been given a defect on its welds at inspection? We grind out, re-weld and prepare for the follow-up inspection. Request a callback.
Our service for this: Custom fabrication and welding →
Free, no-obligation callback

About the author
Tobias Schott
Managing director of Omega Mounting GmbH, Rodgau · more than 20 years of hands-on experience in installation and maintenance
A trained mechatronics technician, working in maintenance, servicing and industrial installation since 2004 – first alongside his father, and with Omega Mounting since 2012: from overhead conveyors in Frankfurt to the crane system in a new-build hall. He plans and leads lifting operations as an appointed person (AP) in data centers and on industrial sites in the Rhine-Main region, trains and examines operators of cranes, mobile elevating work platforms and telehandlers, and is a qualified occupational safety specialist. On jobs abroad he is known as the “German Troubleshooter” – the person you call when a site gets stuck. He learned what quality means from his father, not from a manual: Made in Germany as a standard for his own work, not a label. That is why quality comes first at Omega Mounting – ahead of speed and price. The Technology explained articles cover the equipment and techniques his team uses every day: what counts on site is in them – what only appears in the brochure is not.
 English
 German