
- Technology explained – key term
Commissioning: FAT, SAT and Levels 1 to 5 – the road to handover
By Tobias Schott · 8-minute read · Updated October 2026
Commissioning is the documented proof that a facility has been built as designed and works as designed – and without that proof, no generator, cooling unit or power distribution board goes live in a data center. The word appears in almost every data center tender, in the general contractor’s programme and on the tags hanging from switchgear and generators. If you think of it as simply switching the plant on, you underestimate it: it is a testing process that runs for months, with fixed levels, test scripts and signatures.
For an installation contractor like us, this means that everything we move in, set in place and bolt down is checked again at every level. Below we explain what commissioning is, what Levels 1 to 5 involve, how FAT, SAT, trial runs and acceptance fit together, and what installation contributes.
What is commissioning?
Commissioning is a planned, staged process of testing and evidence. It shows that a facility has been correctly delivered, installed, started up and tested under load – and that it responds as designed together with all other systems. The short form is Cx; German documents often call it “Inbetriebnahme- und Abnahmeprozess”. The difference from a simple start-up is scope: commissioning begins with tests at the manufacturer’s works, ends with handover to operations and records every step.
The process is at its strictest in data center construction, because what a data center sells is availability. You cannot tell by looking whether a standby generator will start and pick up the load when the mains fail – you have to test it.
Key facts
- Definition: Staged, documented proof that a facility has been built and works as designed – from factory testing to handover.
- Also known as: Testing and commissioning (T&C), Cx; in German “Inbetriebnahme” or “technische Abnahme”; in pharma and food production it is related to qualification.
- Terminology: Levels (Level 1 to 5, in some models 0 to 6), tests and test scripts; open items go on the snagging list (punch list), and the process ends in handover.
- Who is involved: Owner or operator, general contractor (GC), an independent commissioning agent (CxA), equipment manufacturers and suppliers, and the specialist trades – including the installation contractor.
- Where you find it: Data centers (power, cooling, fire protection, building management), standby power systems and power plants, production plants, cleanrooms, crane systems.
- Often confused with: Start-up (only one level of it), legal acceptance between client and contractor, and the inspection of work equipment under the German Industrial Safety Ordinance (BetrSichV), which checks safe condition, not system function.
- Result: Signed test records for each level, test status marked on every unit, a closed-out snagging list, handover documentation.
What are commissioning levels 1 to 5?
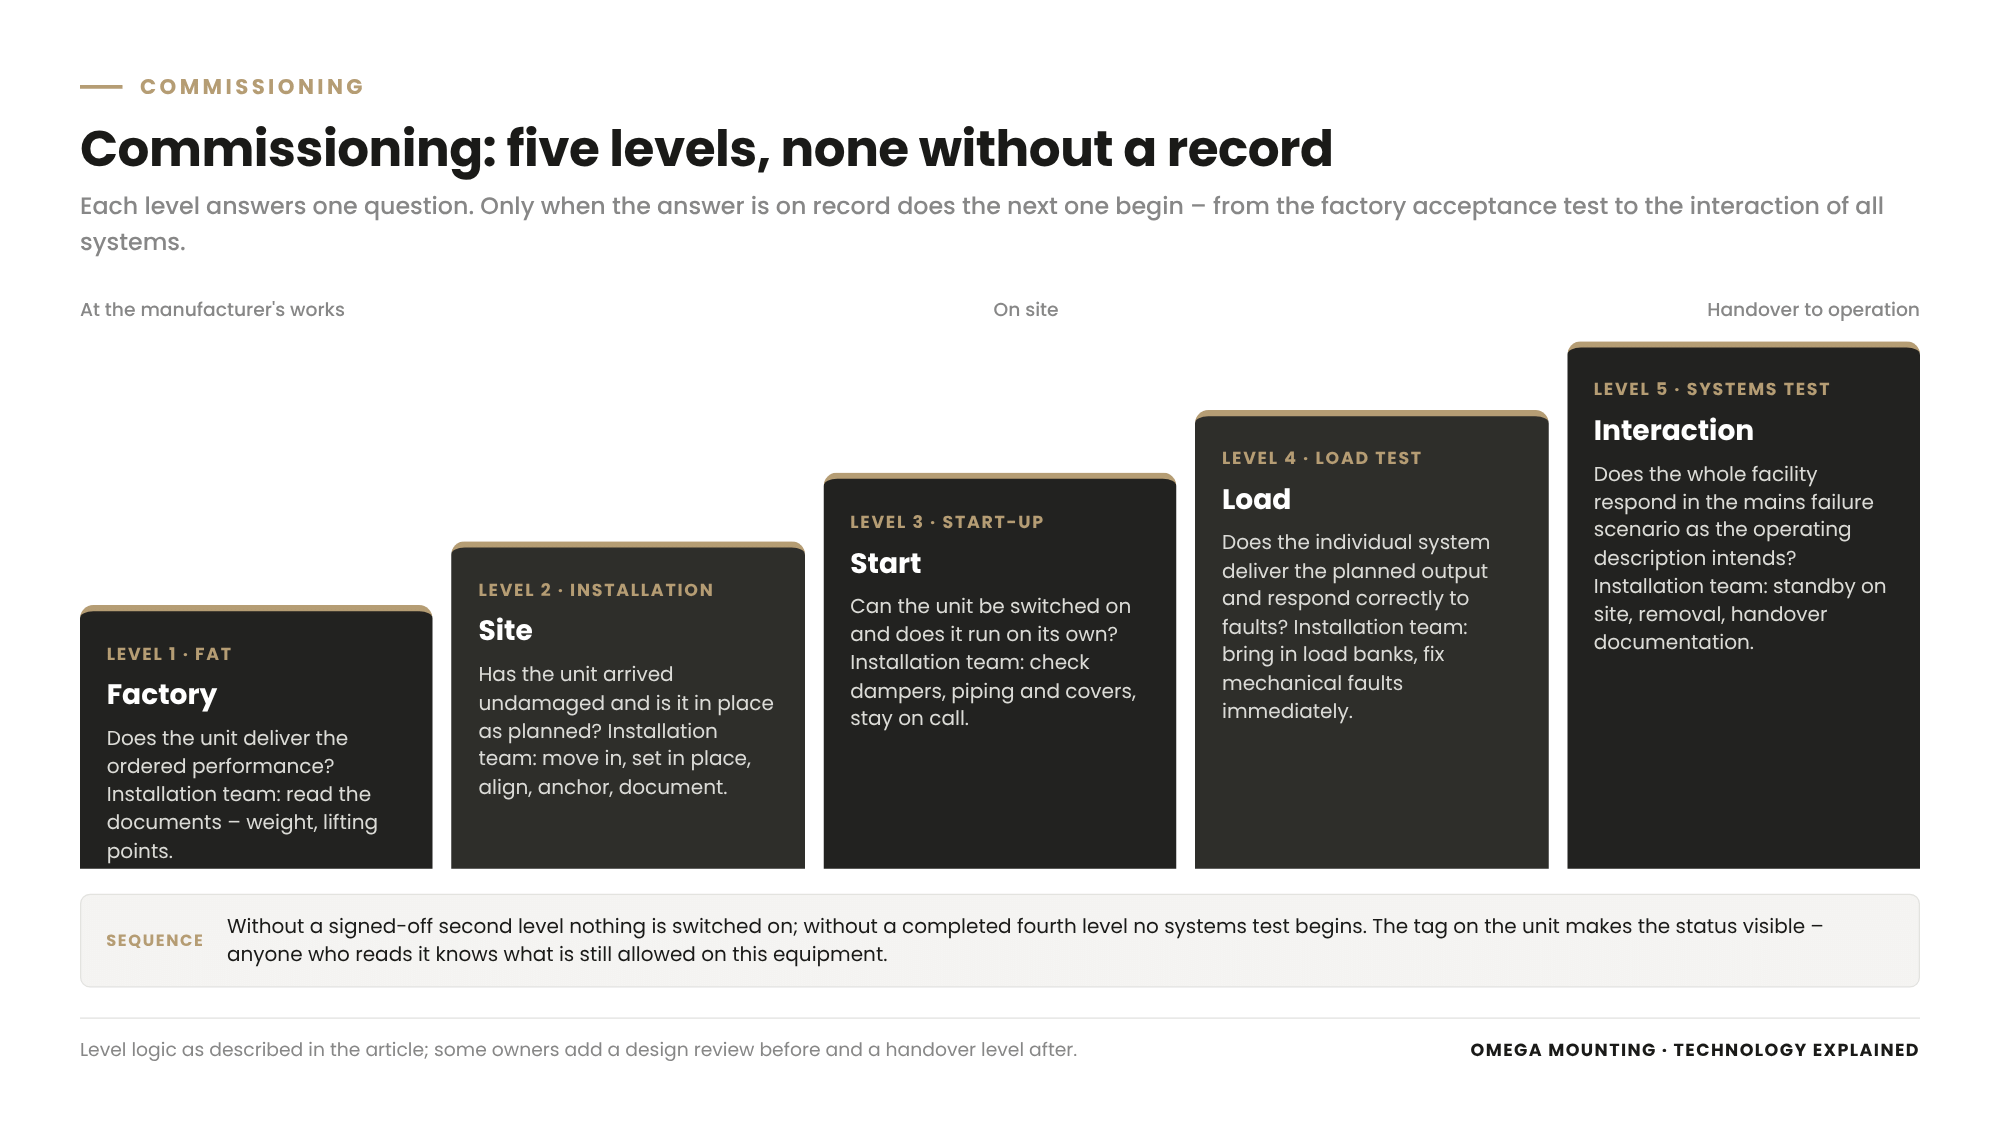
In data center construction, commissioning usually has five levels: Level 1 factory testing, Level 2 delivery and installation, Level 3 start-up, Level 4 performance under load and Level 5 integrated systems testing. Some owners add a design review before (Level 0) and a training and documentation stage after (Level 6); the logic stays the same. Each level answers one question. Only when the answer is documented does the next level begin.
| Level | Typical name | Question answered | What must be in place | Installation role |
|---|---|---|---|---|
| Level 1 – Factory acceptance | Factory Acceptance Test (FAT); when witnessed, Factory Witness Test (FWT) | Does the unit deliver the specified performance at the factory? | Factory test report, approved data sheets, release for shipment | No test duty – we read the documents to know weight, centre of gravity and lifting points for the move-in |
| Level 2 – Delivery and installation | Delivery and installation verification; often split into L2A (red tag: set in place) and L2B (yellow tag: ready to energise) | Has the unit arrived undamaged, and is it set in place as designed? | Goods-in inspection, evidence of placement and anchoring, alignment record, photos | Core level for installation: move in, set in place, align, anchor, record torques |
| Level 3 – Start-up | Start-up and pre-functional test | Can the unit be switched on, and does it run on its own? | Complete installation evidence, isolation and energisation plan, manufacturer’s start-up report | Support: check anti-vibration mounts, pipework and covers; mechanical fitters on call |
| Level 4 – Performance under load | Functional Performance Test (FPT) | Does the individual system deliver its design capacity, and does it respond correctly to faults? | Test script, load bank or heat load, measured data, signed record | Move in and set up load banks, fix mechanical faults immediately |
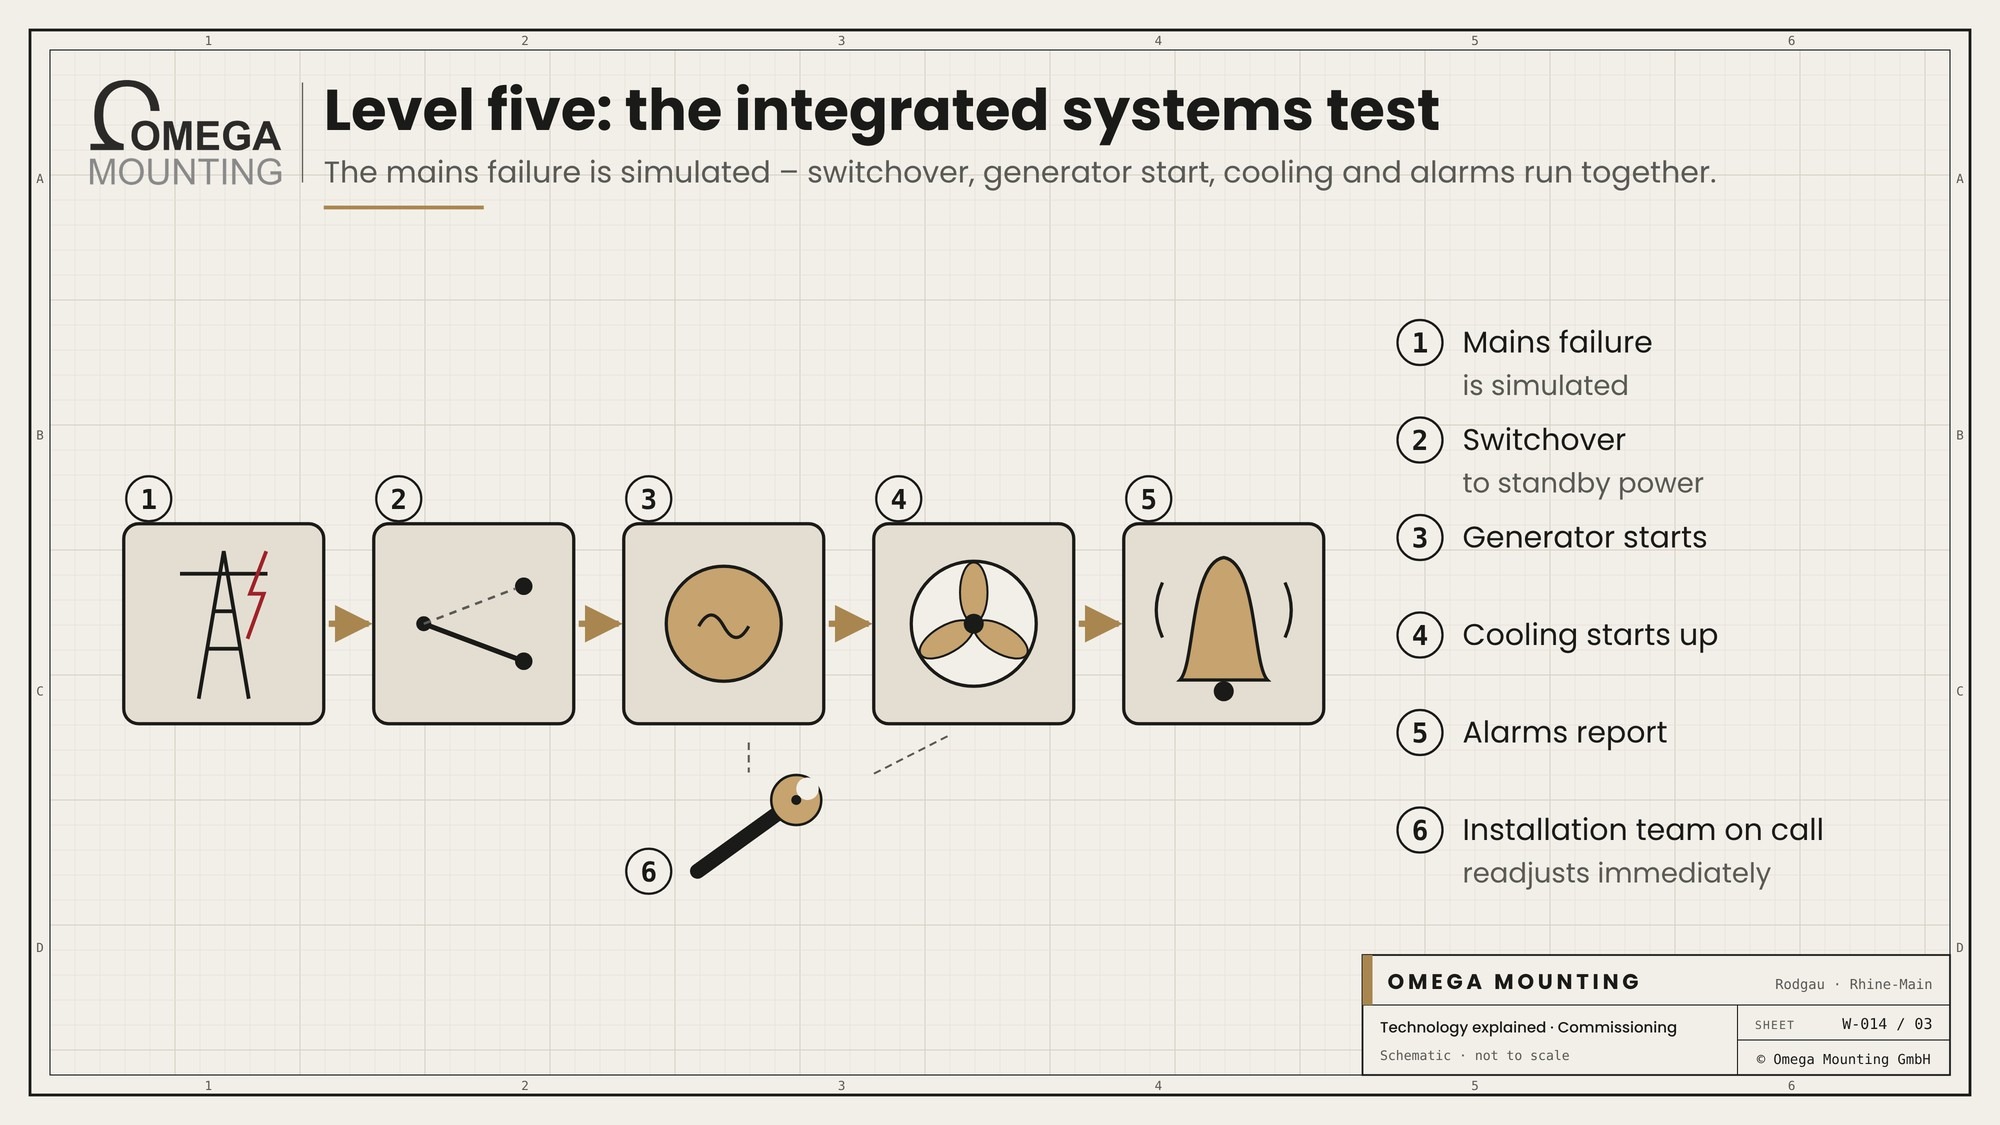
| Level 5 – Integrated systems | Integrated Systems Test (IST) | Does the whole facility respond to a mains failure exactly as the sequence of operations says? | All individual systems signed off, snags closed, operator present as witness | Standby on site, removal of temporary installations, handover documentation |
The defining feature is the fixed sequence: nothing is energised until Level 2 is signed off, and no integrated systems test starts until Level 4 is complete. Many owners show the status on each unit with coloured tags added level by level – commonly red (installed), yellow (ready to energise), green (start-up done), blue (performance tested) and white (IST passed). If you can read the tag, you know what is still allowed on that equipment.
FAT, SAT, trial run, acceptance: how do the terms fit together?
FAT and SAT describe where a test takes place; trial run and acceptance describe its outcome – and all four map onto the five levels. Tenders often list them side by side without explaining how they relate.
- FAT – factory acceptance test. Testing at the manufacturer’s works before the unit is shipped. This is Level 1.
- SAT – site acceptance test. The same test points again after installation, plus everything that can only be checked in place. In the level model, it covers start-up and functional testing.
- Trial run and functional test. A run under defined conditions, such as a standby generator running on a load bank for several hours. This is the core of Level 4.
- Integrated systems test (IST) – Cx L5 (white tag) A mains failure is simulated: transfer, generator start, cooling, alarms – all together. This is Level 5.
- Acceptance under VOB/B or the German Civil Code (BGB). The legal act by which the client accepts the work as compliant with the contract; the transfer of risk and the start of the defects liability period depend on it. It is broadly comparable to practical completion. The technical tests provide the basis for it but do not replace it. This is not legal advice; more in our guide on commissioning and handover.
- Inspection before first use. Occupational safety checks whether work equipment can be operated safely. This runs in parallel with commissioning and is not the same as proving that the system performs.

In practice: a facility can pass all five levels and still not be legally accepted. Keeping the two apart avoids disputes over snags.
What does installation contribute to commissioning?
Installation provides the evidence that the equipment sits exactly where the design says – without that evidence, the process does not get past Level 2. Our contribution is mechanical and documentary:
- Installation evidence. Position, alignment, anchoring, clearances to walls and adjacent units, photos before the covers are closed.
- Torque and installation records. Anchors, flanges and frame bolts with torque value and a visible torque mark, so the inspector can see what has been tightened.
- Closing out the snagging list. Snags from the walk-downs – a missing cover, an open cable tray, scratched paint – are closed by a deadline, with evidence of completion.
- Test support. During start-up, load testing and the integrated systems test we keep mechanical fitters on call. If an anti-vibration mount, an exhaust flange or a radiator bracket causes trouble, someone has to be there to fix it straight away.
- Handover documentation. Records, as-built drawings, material certificates and anchor documentation, bundled for handover.

We are just as clear about where our scope ends: insulation tests on the system are carried out by our own qualified electricians, protection settings in the building network remain with the operator, and starting the control system with the manufacturer or system integrator. We handle the mechanical work and the system electrics and document both so that the next level can build on it – for international clients often in English.
What we pay attention to
In commissioning, the course of the installation work is decided long before the first test. This is what we keep an eye on:

- Factory documents before the move-in. Weight, centre of gravity, lifting points and transport restraints are in the Level 1 documents. We read them before the crane arrives.
- Document on the same day. Photos and records are made while the cover is still open – not a week later from memory.
- Make torque visible. Every documented bolted joint carries its torque mark. What the inspector cannot see, they have to question.
- No hands-on without a permit. If a unit carries the tag of a higher level, we only touch it with authorisation and a permit to work. One loosened cover can invalidate a completed test.
- Close snags with evidence. Every snag gets a before-and-after photo and a date.
- Plan standby for the test phase. Load and integrated systems tests follow the test programme, not our normal working hours. Being there when something sticks prevents delays across the whole programme.
Where we use it
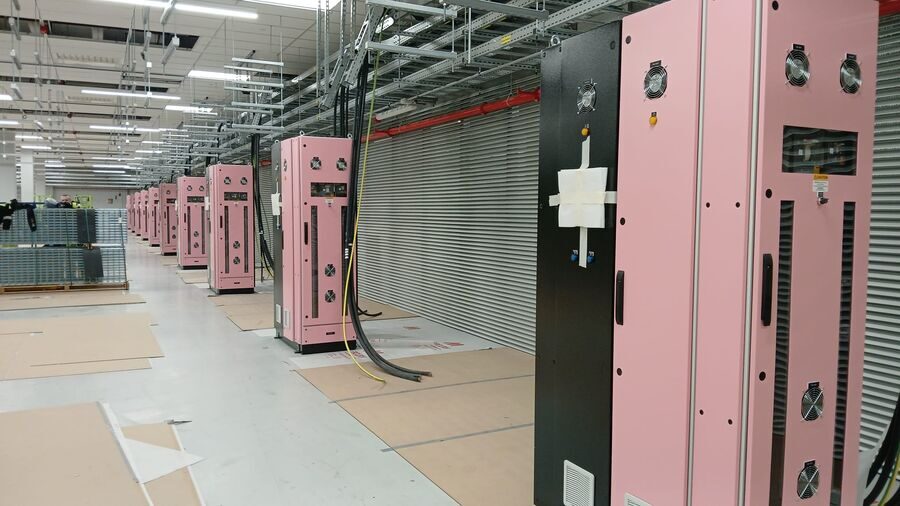
We mostly meet commissioning in data centers in the Rhine-Main region, at every one of the five levels. In Frankfurt am Main, a team of nine unloaded five heavy transports with generators and load banks in one working day. A 220-tonne-class mobile crane set them into a multi-storey steel structure – the load banks are the test equipment for Level 4. In Offenbach am Main, three fitters installed twelve double turbo silencers above the standby generators, followed by performance and noise testing under full load. For 160 power distribution cabinets in eight data halls, our team laser-surveyed and marked every position, before each cabinet was aligned and handed over to the electrical contractor. For our wider data center work, see our page Data center construction.
More technology explained
Technology explained
the plant most often at the centre of load testing and the integrated systems test.
Technology explained
the authorisation required before any work on a tagged unit.
Guide
the guide with the documentation checklist for installation work.
Need fitters who know this process?
Planning a project that requires commissioning at every level, and need fitters who know the process and document their work ready for inspection? We move the equipment in, set it in place and support the tests through to handover. The quickest way is a callback – tell us briefly about the project, the equipment and the timeframe.
Free, no-obligation callback

About the author
Tobias Schott
Managing director of Omega Mounting GmbH, Rodgau · more than 20 years of hands-on experience in installation and maintenance
A trained mechatronics technician, working in maintenance, servicing and industrial installation since 2004 – first alongside his father, and with Omega Mounting since 2012: from overhead conveyors in Frankfurt to the crane system in a new-build hall. He plans and leads lifting operations as an appointed person (AP) in data centers and on industrial sites in the Rhine-Main region, trains and examines operators of cranes, mobile elevating work platforms and telehandlers, and is a qualified occupational safety specialist. On jobs abroad he is known as the “German Troubleshooter” – the person you call when a site gets stuck. He learned what quality means from his father, not from a manual: Made in Germany as a standard for his own work, not a label. That is why quality comes first at Omega Mounting – ahead of speed and price. The Technology explained articles cover the equipment and techniques his team uses every day: what counts on site is in them – what only appears in the brochure is not.
Frequently asked questions
Level 2, the delivery and installation level. We move equipment in, set it in place, align and anchor it, and record torques and photos. In models that split Level 2, our scope ends at the red tag (L2A): the unit is rigged into place, properly anchored and inspected. From Level 3 onwards we keep mechanical fitters on call during start-up, load and integrated systems tests.
Yes, in some owners’ models. Level 0 is the design review before construction, checking that the design can be commissioned. Level 6 follows the integrated systems test and covers training and documentation for handover to operations. Levels 1 to 5 stay the same: factory testing, delivery and installation, start-up, functional performance testing and integrated systems testing.
 English
 German